Fast-Cycling vs. Washdown Equipment: Which Pneumatic Cylinder Features Matter?
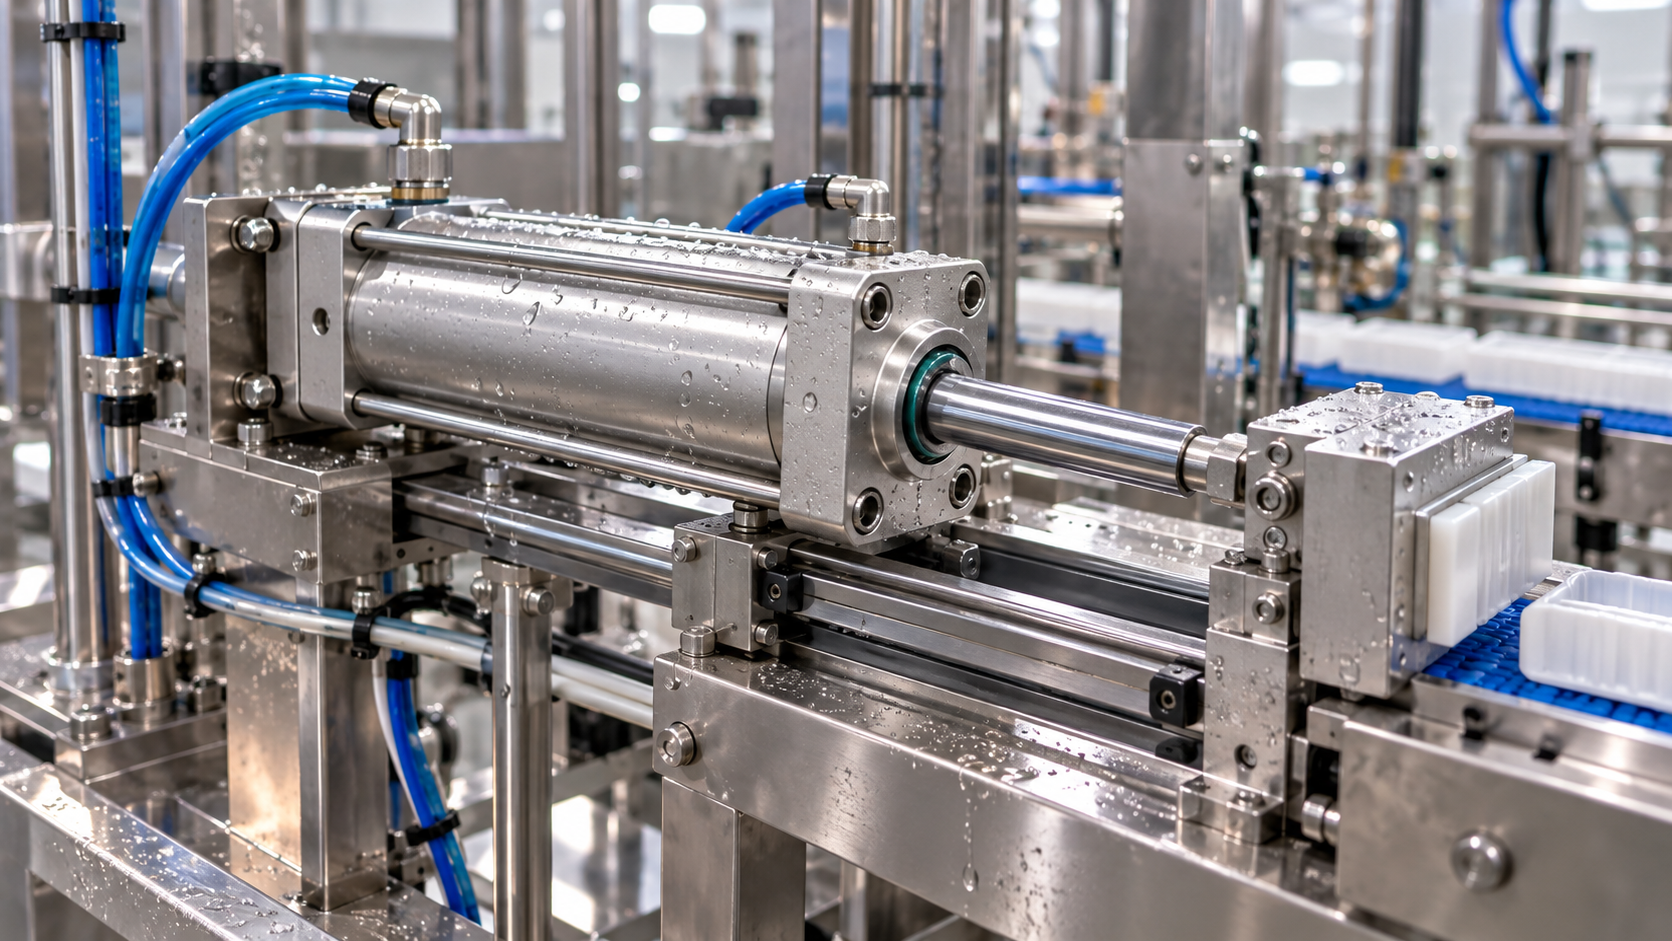
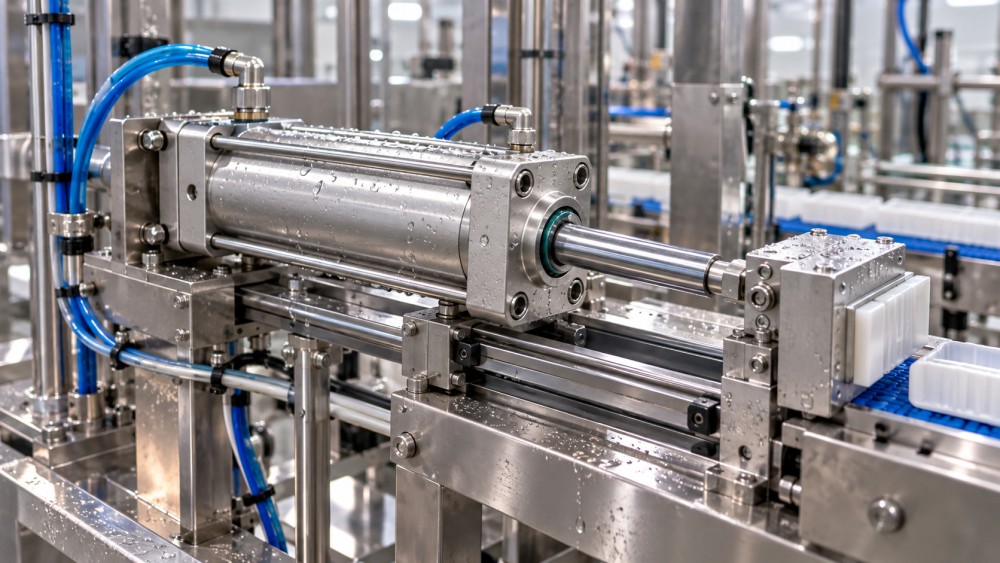
A pneumatic cylinder that runs smoothly on a high-speed assembly line may struggle after repeated chemical washdowns. Conversely, a corrosion-resistant actuator can survive cleaning yet still become the bottleneck in a fast packaging machine. The difference is rarely just bore size or stroke.
For technical evaluators, choosing pneumatic cylinders for fast-cycling or washdown equipment means identifying which failure mechanisms will dominate. Rapid motion puts cushioning, seal friction, airflow, and alignment under scrutiny. Washdown service shifts attention toward chemical compatibility, liquid ingress, and surfaces that can actually be cleaned. Where these conditions overlap, neither a standard industrial cylinder nor a stainless steel housing alone settles the decision.
Start with the operating profile, not the cylinder catalog
“High speed” and “washdown duty” are incomplete specifications. A short-stroke actuator making frequent movements presents a different challenge from a long-stroke cylinder accelerating a heavy carriage. Likewise, occasional water spray is not equivalent to daily hot cleaning with alkaline detergent and a sanitizer.
Before comparing products, document the conditions that suppliers must evaluate:
- Motion: stroke, cycles per minute, travel time in each direction, dwell time, and required positioning repeatability.
- Load: moving mass, process force, orientation, external guidance, and potential side loading.
- Air supply: minimum available pressure during operation, valve flow capacity, tubing length, and compressed-air quality.
- Cleaning exposure: chemical identity, concentration, temperature, contact time, rinse method, and cleaning frequency.
- Installation: mounting orientation, drainage, access for maintenance, sensor locations, and surrounding splash zones.
This record does more than improve sizing. It creates a common basis for supplier quotations, preventing one vendor from assuming a lightly loaded, dry application while another prices for aggressive cleaning and continuous operation.
Which features deserve priority?
The priorities differ, but they are not independent. A chemical-resistant seal with higher friction can change low-pressure motion. A protective cover can shield a rod while introducing a difficult-to-clean cavity. Evaluate each feature as part of the installed assembly.
For fast cycling, control the stop as carefully as the stroke
Cushioning must match kinetic energy
Maximum piston speed is not a complete performance specification. The cylinder must also decelerate the moving load without repeated hard impacts or excessive settling time. Kinetic energy follows E = ½mv², so doubling speed quadruples the energy that must be managed for the same moving mass.
Check the manufacturer's permissible load-and-speed envelope and cushioning limits. Include the tooling and other translated components, not merely the workpiece. Gravity and external forces can add to the stopping demand in vertical or driven arrangements.
Adjustable pneumatic cushioning offers tuning flexibility, but it needs sufficient deceleration distance. Excessively restrictive adjustment may produce a slow final approach or unstable stopping behavior. Fixed or self-adjusting cushioning may simplify setup within its intended operating range. Where cylinder cushioning is insufficient, an externally rated shock absorber or controlled motion profile may be necessary.
Airflow can defeat an otherwise correct selection
A correctly sized cylinder may still move too slowly because the valve, fittings, flow controls, or exhaust silencer restrict flow. Long tubing adds volume and delays pressure changes; an undersized exhaust path can limit speed even when inlet pressure appears adequate.
Compare valve flow characteristics using a consistent rating basis, then assess the complete circuit at the required cycle rate. Pressure should be checked near the actuator during motion, not only at the compressor or regulator. Simultaneous demand from neighboring actuators may reveal a supply problem that a single-cylinder bench test misses.
Meter-out control is commonly used to regulate pneumatic cylinder speed, but the correct arrangement depends on load behavior and circuit design. Quick-exhaust valves can improve response in suitable applications; they also introduce noise, placement, and environmental-exposure considerations.
Friction and alignment determine whether speed stays repeatable
Low-friction seals can reduce breakaway resistance and improve motion consistency, particularly at lower pressures. However, low initial friction does not establish long service life. Ask how seal performance changes with temperature, duty cycle, air quality, and lubricant condition.
Side loading deserves equal attention. A piston rod is not a substitute for a linear guide. Misalignment can accelerate rod-bearing and seal wear, turning a promising speed test into an early maintenance problem. Use suitable external guidance or a guided actuator when the tooling imposes lateral forces or moments.
For washdown, inspect beyond the stainless steel label
Stainless steel construction is useful, but it is not a universal guarantee against corrosion or contamination. Material grade, surface finish, crevices, chemical exposure, and assembly details all influence service performance.
Specify the cleaning chemistry precisely
Supply the cylinder manufacturer with cleaning-product information and the actual dilution, temperature, exposure time, and rinse sequence. “Food plant cleaner” or “sanitizer resistant” is too vague for a meaningful compatibility assessment.
Seal materials involve trade-offs. EPDM may suit certain hot-water and cleaning exposures, while NBR or FKM may be preferable for other media and operating conditions. None is universally suitable. Compatibility depends on the particular compound, not simply the polymer family, and must include the compressed-air lubricant where one is used.
The same review should cover rod wipers, cushioning seals, static seals, lubricants, adhesives, sensor cables, and connector materials. A resistant cylinder body cannot compensate for a cable jacket that cracks or a wiper that swells after cleaning.
Cleanability is a geometry question
Exposed threads, tie-rod recesses, narrow mounting gaps, and horizontal ledges can retain soil or cleaning liquid. Rounded profiles and accessible surfaces generally make cleaning easier, but inspect the mounted assembly rather than an isolated product photograph.
Rod bellows illustrate the trade-off. They may protect against direct contamination, yet folds can trap residue and complicate inspection. Their use needs application-specific justification, especially where hygienic cleaning is required.
Corrosion resistance and hygienic suitability are separate claims. A cylinder can resist cleaning chemicals while remaining difficult to clean. For equipment with formal hygiene requirements, request evidence relevant to the intended application rather than accepting general “washdown-ready” wording.
Ingress protection does not prove chemical resistance
Check exactly which components carry an ingress-protection rating and under what conditions. A rated magnetic sensor does not automatically make its connector, cable junction, valve, or complete actuator installation equally protected. Water-ingress tests also do not establish resistance to detergent or sanitizer exposure.
Consider how water could enter through ports, exhaust arrangements, damaged tubing, or exposed fittings. Where appropriate, locate valves and exhaust outlets outside the direct wash zone and provide suitable routing and drainage. Any protective arrangement must preserve the airflow required for normal operation.
When rapid motion and washdown share the same machine
A packaging actuator beside a filling station may face both continuous cycling and daily cleaning. Here, the selection process should not alternate between two separate checklists; it should test how the requirements interact.
For example, changing to a chemically compatible seal may alter breakaway force. A remote valve arrangement may reduce washdown exposure but increase tubing volume and response time. An external shock absorber may solve impact loading while adding surfaces and mounting details that require cleaning assessment.
Establish non-negotiable environmental requirements first, then verify motion performance within those constraints. If no conventional cylinder arrangement meets both, reconsider placement, guarding, guidance, or actuator architecture rather than repeatedly upgrading individual components.
Size for available force, then check the consequences
Theoretical extension force is pressure multiplied by piston area. Retraction force is lower because the rod reduces the effective area. Actual usable force also reflects friction, exhaust-side backpressure, pressure losses, and dynamic conditions.
As an illustration, a 32 mm bore has a piston area of approximately 804 mm². At a differential pressure of 0.6 MPa, its theoretical extension force is about 482 N. That is not a guaranteed working force: the real application must account for losses and the required acceleration.
Use the minimum credible operating pressure and an application-appropriate force margin agreed with the supplier. Avoid solving every uncertainty with a larger bore. Oversizing increases air demand and can require larger valves and tubing; faster motion may also increase stopping demands. For long strokes under compression, verify rod buckling limits and mounting suitability separately.
What to request before approving a supplier
A useful technical comparison separates documented capability from catalog shorthand. Ask shortlisted suppliers for:
- Application-specific sizing: force, velocity, cushioning, mounting, and rod-load checks using your operating profile.
- Endurance-test conditions: load, stroke, speed, pressure, air quality, failure criteria, and maintenance performed during testing.
- Material details: wetted and exposed metals, seal compounds, lubricants, and written compatibility guidance for the cleaning process.
- Assembly-level limitations: sensor and connector ratings, permitted cleaning conditions, installation restrictions, and excluded exposures.
- Service information: seal-kit availability, replacement procedure, lubrication requirements, and inspection guidance.
Cycle-life claims are useful only when their test conditions resemble the intended duty. Likewise, a chemical-compatibility chart is a screening aid, not proof that the assembled cylinder will withstand every cleaning sequence.
Make the final decision under representative conditions
For a fast-cycling trial, record travel time in both directions, pressure behavior, end-stop impact, leakage, and repeatability after sustained operation. For washdown evaluation, reproduce the actual cleaning sequence and inspect for corrosion, seal changes, trapped liquid, and sensor faults. A few successful cleaning cycles cannot establish long-term life, but they can expose obvious mismatches.
Where both duties apply, test motion again after cleaning—not just before it. That is when increased friction, ingress, or connection problems may become visible.
The strongest selection is not necessarily the fastest cylinder or the one with the most stainless steel. It is the actuator-and-circuit combination whose motion limits, material compatibility, cleanability, and maintenance requirements match the machine's real operating conditions. That evidence gives technical evaluators a firmer basis for approval than either headline speed or a washdown label alone.
Related News
- Fast-Cycling vs. Washdown Equipment: Which Pneumatic Cylinder Features Matter?Time : Oct 30, 2026
- Industrial Air Cylinder Uses in Clamping, Material Handling, and PackagingTime : Oct 25, 2026
- Choosing an Air Cylinder Supplier in the Middle East: Stock, Lead Times, and SupportTime : Oct 22, 2026